Cable carriers for SMT and PCB equipment
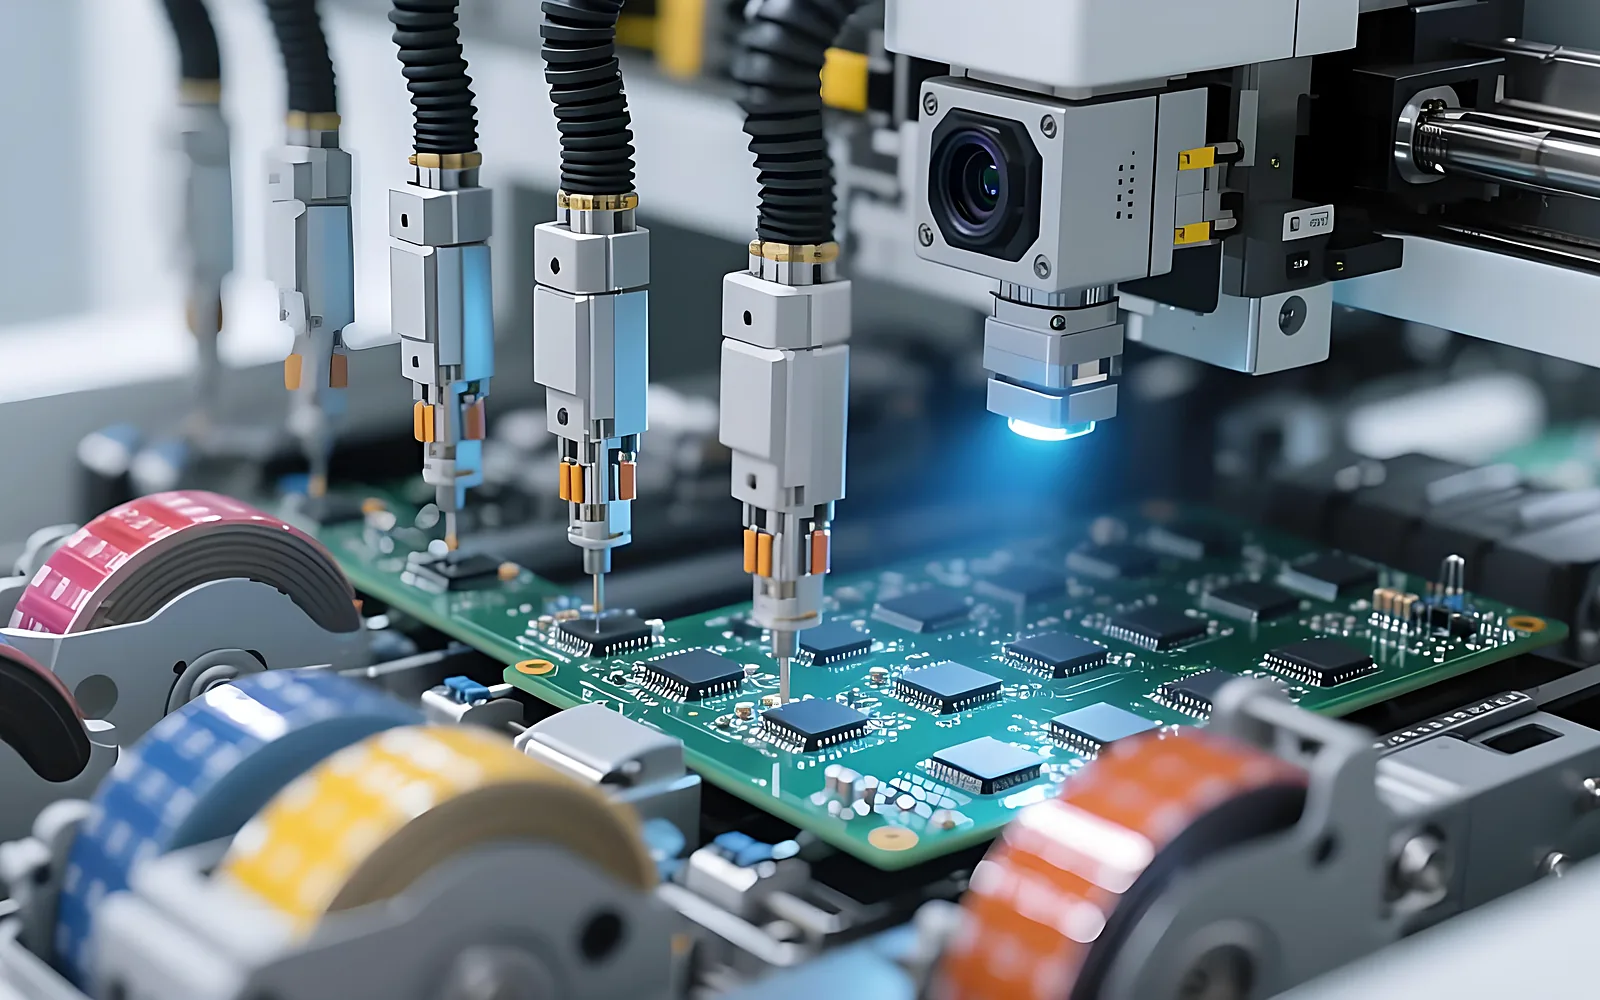
Cable carrier selection for SMT and PCB equipment: cleanliness, short-stroke vibration, cable layering, bend radius and the WWC range.
Ask anyone in an SMT hall why they are looking at cable carriers, and eight times out of ten it is because a pick-and-place head has chewed through its cables, or a cleanliness audit came back over the particle limit. SMT axes are short-stroke and very fast, and the cables in them are thin signal lines, optical fibres and air lines, often running inside a controlled environment. A standard nylon carrier will work for a few months, then start shedding particles, rattling, and throwing signal faults.
This article walks the real machine locations on an SMT line: where a carrier is actually needed, how SMT duty differs from general machine-tool duty, how to hold cleanliness, how to select for short stroke and high cycle rate, which WWC inner height fits, and ends with a quotation checklist.
Where a carrier is actually needed on an SMT line
A complete SMT line, from loader to depaneliser, has plenty of moving parts. Only the ones that carry cables and move constantly need a carrier:
- The X-Y gantry and placement head of the mounter: short stroke, usually a few hundred millimetres, high acceleration, dense cable bundle. This is the most demanding location.
- Feeder platform and change carts: move forward and back during replenishment, mostly signal and power.
- Squeegee and vision module of the solder paste printer: short stroke, high cycle rate, and the stencil sits directly underneath, so any shedding lands on the print.
- Camera beam of AOI and SPI machines: sensitive to repeatability, and carrier vibration goes straight into the image.
- Lift and transfer mechanisms of loaders, buffers and depanelisers: mostly vertical or short horizontal motion in tight space.
- Transfer section at the reflow oven inlet and outlet: elevated temperature, so material temperature rating is a hard requirement here.
Fixed transfer rails and internal frame wiring ducts do not need a carrier. Counting how many axes actually move is more useful at quotation time than asking for a price first.
How SMT duty differs from general machine-tool duty
Four differences mean you cannot simply reuse machining-centre experience:
- Short stroke, fast cycle. A machining-centre carrier may travel several hundred millimetres a few times a day. A mounter axis reverses every second. Over a year the cycle count can be an order of magnitude higher, and wear accumulates by cycle count.
- Thin cables, many of them. One power cable plus a dozen signal cables, two fibres and an air line is normal. Thin cables tolerate less bending and are more sensitive to bend radius.
- Cleanliness is a hard requirement. Shedding on a machining centre is ignored; shedding in an SMT hall is counted by a particle counter.
- Very little space. The enclosure is already crowded, and the available mounting height is often only tens of millimetres.
The conclusion: an SMT carrier should be small, light, low-shedding and low-clearance, not merely strong. Applying heavy-duty margins makes links heavier, raises inertia and worsens vibration.
Cleanliness: where the particles come from
Particles in a cleanroom have many sources. The share contributed by the carrier comes mainly from three places:
- Sliding friction between links: the dominant source. Links rub against each other as they bend and straighten, and the abraded material becomes particles.
- Friction between cable jacket and carrier wall: cables creep inside the channel and the jacket wears.
- Outgassing and ageing of the material itself: ordinary nylon fuzzes after long bending, and fuzzing means shedding.
Three corresponding actions:
- Choose the right material. For cleanroom use, TPU rather than ordinary nylon; its wear behaviour and low outgassing suit the duty. The CNWSL WWC series uses TPU and is rated -20℃ to 120℃.
- Control cable movement inside the channel. If cables can creep freely, the friction surface keeps changing. Dividers and vertical separators fix the bundle in layers, reduce creep, and wear follows.
- Do not push the bend radius to its limit. A smaller radius means a larger link articulation angle and a longer friction path. One step of margin helps both shedding and life.
Cleanliness classes are defined in ISO 14644-1:2015, which classifies by airborne particle concentration from 0.1 µm to 5 µm. The "Class 100" still found on old drawings comes from the withdrawn US Federal Standard 209E and corresponds roughly to ISO Class 5 under ISO 14644-1. Ask the customer which scheme they use before quoting, and never treat Class 100 and ISO 100 as the same thing; the two numbers are three orders of magnitude apart.
Short stroke, high cycle rate: pitch and clearance
Short stroke is what makes SMT carriers special, and it is where selection most often goes wrong.
Problem one: the stroke is too short to complete the bend. A carrier needs a full 180° bend arc in normal operation. If the stroke is shorter than the space that arc requires, the chain oscillates in a half-bent state, links stay loaded mid-articulation, and wear concentrates on a few links. The failure looks like "one link wore through far too early", but the cause is a mismatch between stroke and bend radius.
The check is simple: look at stroke and bend radius together, and make sure the stroke allows at least one complete bend-straighten cycle. If the stroke really is very short, reduce the bend radius or use a design that does not require a full arc.
Problem two: clearance becomes vibration. Links always have fit clearance, and clearance times the number of links is the accumulated play. On a long stroke the play averages out; on a short stroke with high acceleration it appears as an impact at every reversal. On a machine that positions to micrometres, that impact reaches the frame.
Three things you can do:
- Choose a series with a smaller pitch, so the same clearance is distributed over shorter links and accumulates less.
- Reduce the load inside the channel: split thin cables into separate compartments instead of filling one cavity.
- Fix both end connectors rigidly so the chain cannot find its own position.
Speed and acceleration limits follow a separate calculation, covered in cable carrier speed and acceleration limits.
Inner width and layering: how many cables per cavity
On SMT equipment, inner width is not set by what fits, but by what still moves after it fits.
- Fill ratio: total cable cross-section, including the outer envelope, over the carrier inner cross-section. Keep it below 60%. Above that, cables have no lateral room and press against each other while bending.
- Layering: run power, signal and fibre in separate compartments. Interference matters, but the more practical issue is thick cables pushing thin ones against the wall.
- Fibre on its own: optical fibre allows a much larger bend radius than cable and dislikes side load. Mixed in with thick cables, one bend can exceed its limit.
The calculation itself is in how to choose cable carrier inner width.
Bend radius: work back from the cables
The order cannot be reversed: cables first, then R, then check whether the frame has room.
- Cable bend radius is normally given as a multiple of outer diameter, and the multiples for power cable, signal cable and fibre are completely different, with fibre the largest.
- The carrier bend radius must exceed the lower limit of the most demanding cable in the bundle.
- With R fixed, re-check mounting height: a larger R takes more height in the bend, and inside an equipment enclosure this is often what makes a layout impossible.
The full method is in how to calculate cable carrier bend radius.
The WWC cleanroom series by inner height
The CNWSL cleanroom carrier is the WWC series: TPU, rated -20℃ to 120℃, in five inner heights:
| Series | Inner height | Inner width | Available bend radii |
|---|---|---|---|
| WWC15 | 15 mm | 25 mm | R40 / R50 / R60 / R70 |
| WWC18 | 18 mm | 32 mm | R40 / R50 / R60 / R70 |
| WWC22 | 22 mm | 40 mm | R40 / R50 / R60 / R70 |
| WWC28 | 28 mm | 65 mm | R40 / R60 / R70 / R90 |
| WWC35 | 35 mm | 65 mm | R60 / R70 / R90 |
Rough mapping to SMT duty:
- Placement-head signal bundle, AOI camera beam → WWC15 / WWC18, short stroke and thin cables.
- Printer squeegee, feeder platform, loaders → WWC22 / WWC28.
- Depanelisers, or where an air line or heavier power cable is routed → WWC35.
This is order-of-magnitude guidance only; the actual size comes from the cable list. Product page: cleanroom cable carrier WWC series; datasheets under downloads.
Installation details that get missed
- Horizontal or vertical mounting. Vertical mounting is common on SMT equipment for lift and buffer mechanisms. The chain's own weight then acts directly on the bend, and unsupported length behaves differently from horizontal mounting. Do not reuse horizontal figures.
- Fixed-end position. On short-stroke machines the fixed end is often dictated by the frame, but make sure the chain is neither pulled straight nor bottomed out at either limit. Allow one to two links at each end.
- Guide channel or not. Usually unnecessary for short stroke, but if the bundle is heavy or sees lateral force, a short guide is cheaper than a later structural change.
- Equipotential bonding of connectors and mounting brackets. SMT halls have electrostatic requirements. IEC 61340-5-1:2024 is the current edition and specifies how an ESD control programme is established and maintained. The carrier is not an ESD control device, but bonding of metal connectors and brackets should be handled during assembly, not left as a retrofit.
Machine safety requirements are in IEC 60204-1:2016 for routing and fixing of cables on moving parts, and ISO 12100:2010 for risk assessment methodology. Where an air line runs in the chain, its allowable bend radius is usually larger than that of cable; see ISO 4414:2010 rather than applying cable figures.
Six common mistakes
- Ordinary nylon carrier in a clean area, particle count out of limit within months.
- Short stroke paired with a large bend radius, the arc never completes and individual links wear through early.
- Fill ratio pushed to 80%, cables press together while bending and jackets fail.
- Fibre and power cable in the same cavity; one bend exceeds the fibre limit.
- Vertical mounting using horizontal unsupported-length data.
- Comparing carrier price only, without counting replacement downtime, which dwarfs the part cost on an SMT line.
Seven items to put in the enquiry
| Item | What to state |
|---|---|
| Location | Placement head / camera beam / lift mechanism / transfer section |
| Mounting | Horizontal / vertical / side |
| Stroke | Effective stroke in mm, plus cycles per minute |
| Acceleration | Peak acceleration, or cycle time if unknown |
| Cable list | Count, outer diameter, type (power / signal / fibre / air) |
| Cleanliness class | Customer scheme (ISO class or Class) and test standard |
| Space limit | Mounting height, available length, existing guide channel |
With these seven stated, the reply should be a specific series, inner width, bend radius and link count, not a line about stock availability.
Supply and validation
CNWSL manufactures in Tiancheng Street, Yueqing, Zhejiang, with its own production capacity and in-house tooling; factory visits can be arranged. Sales is handled through our Changzhou office. We hold IATF 16949 and can provide the system documentation.
One honest caveat: cleanroom performance depends strongly on the actual cables, stroke and acceleration, so a datasheet is only a first filter. Run a small batch with your real cable set and observe shedding and wear for a few months before committing to volume. That is more reliable than any table comparison.
Related reading
- Cleanroom cable carrier selection guide
- Eight-step cable carrier selection
- Cable carrier speed and acceleration limits
To size a carrier for your SMT equipment, contact us or take the WWC datasheets from downloads.